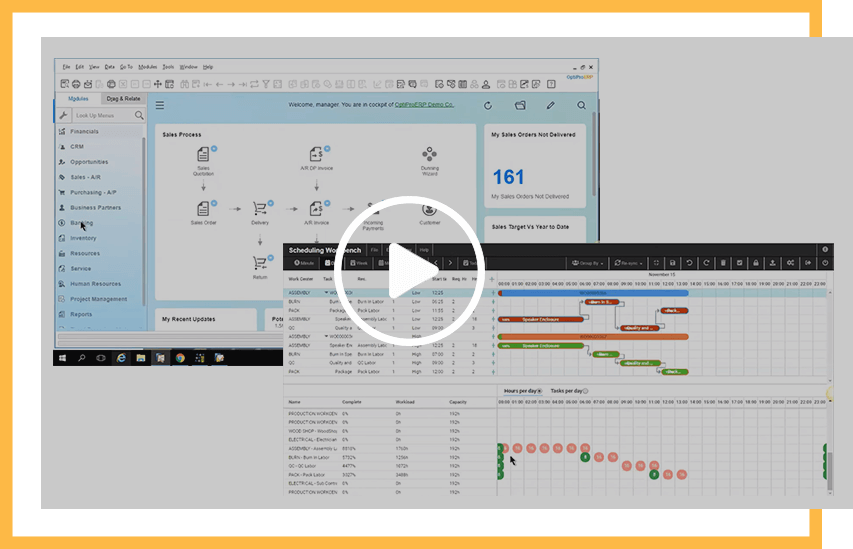
Our vision is to harness advanced ERP management technology to create a fully synchronised manufacturing ecosystem in which warehouse inventory levels are seamlessly aligned with shop-floor production in real time. By integrating inventory intelligence with operational execution, we enable greater supply chain efficiency, precise stock tracking, automated replenishment, and cohesive coordination between production and warehouse teams. This unified approach empowers businesses to operate with agility, respond proactively to demand fluctuations, and build long-term operational resilience.
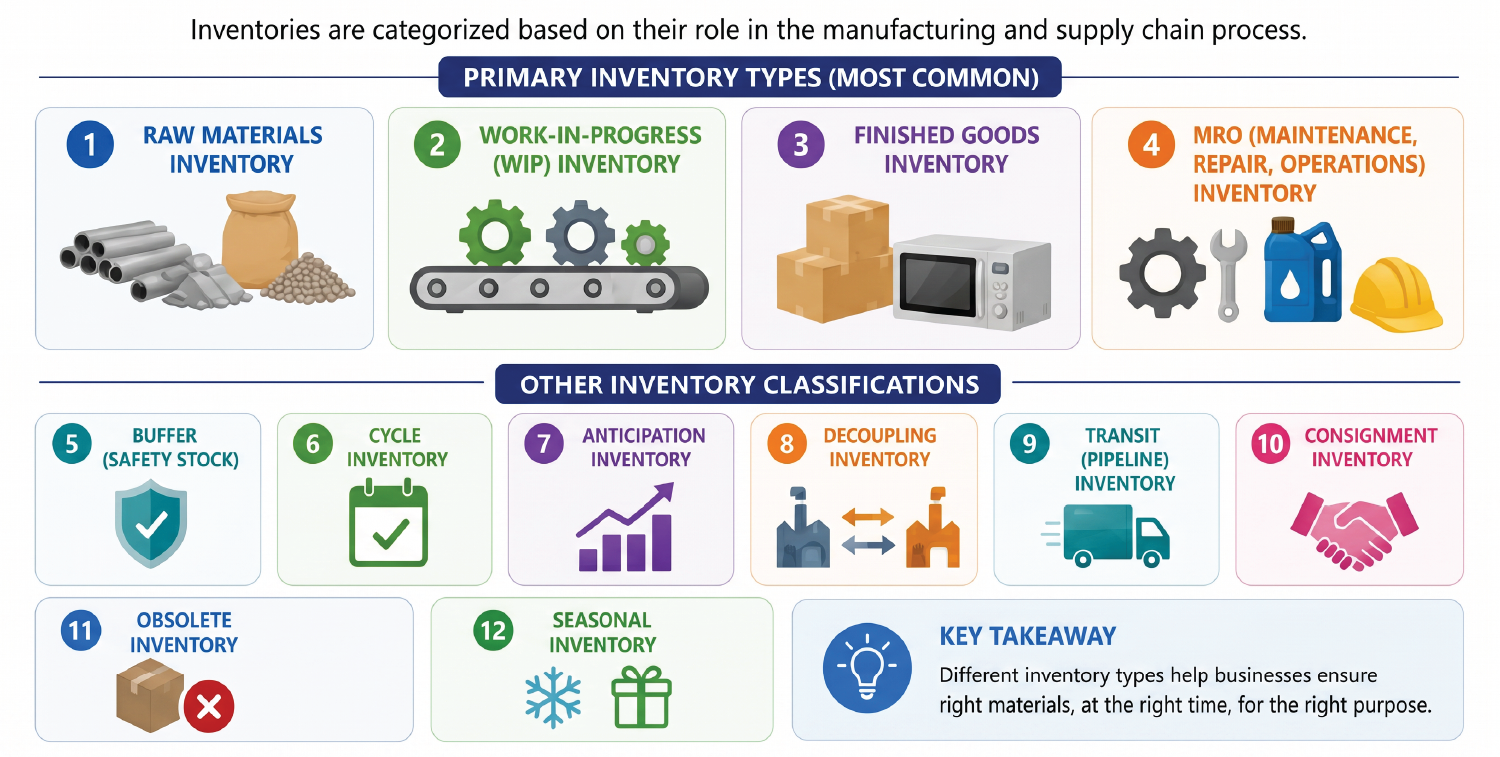
‘Inventory’ refers to the collection of goods, raw materials, and physical stock that is tracked, controlled, and valued to ensure seamless production planning and enhanced customer satisfaction.
The earliest form of inventory management dates back over 50,000 years when people used “tally sticks” to count. And, approximately 4,000 years ago, clay tokens were used to keep track of livestock.
Inventory management is a systematic approach to optimising stock levels by providing real-time visibility and improving working capital efficiency. It is a method to re-engineer workflows and automate processes so that firms can adopt a proactive approach in day-to-day business operations, thereby minimising lead times, achieving better operational efficiency, ensuring service continuity, and improving customer satisfaction and market performance.
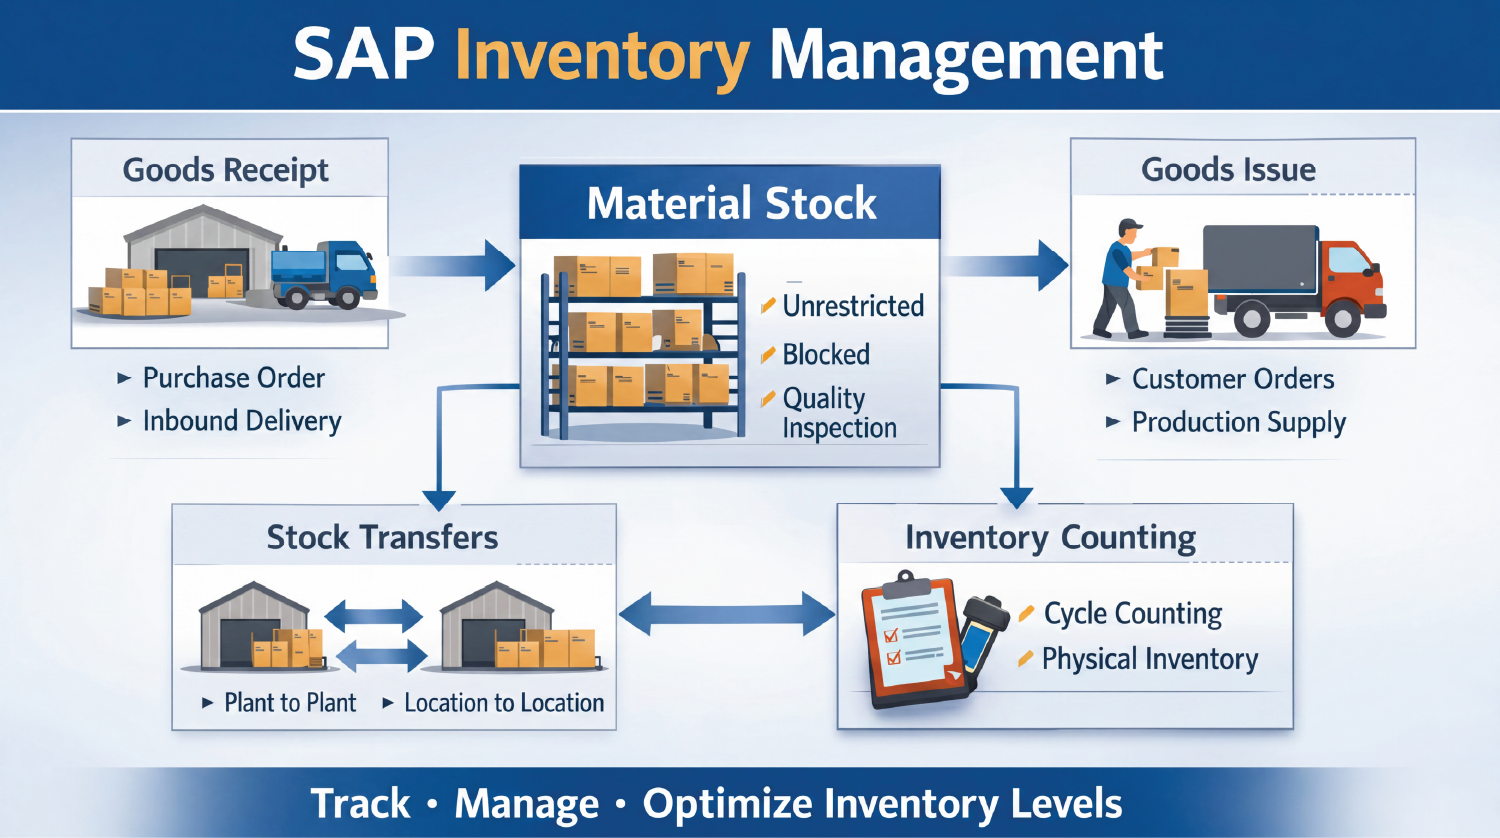
An ERP-based system delivers a set of core capabilities that support integrated business operations, including the following:
Ensures accurate recording and verification of incoming materials against purchase orders.
Facilitates seamless movement of inventory across warehouses and bin locations while maintaining real-time visibility.
Provides end-to-end traceability for regulatory compliance, quality assurance, and recall management. It also enables genealogical functionality.
Optimizes warehouse organization with precise location tracking and improved picking accuracy.
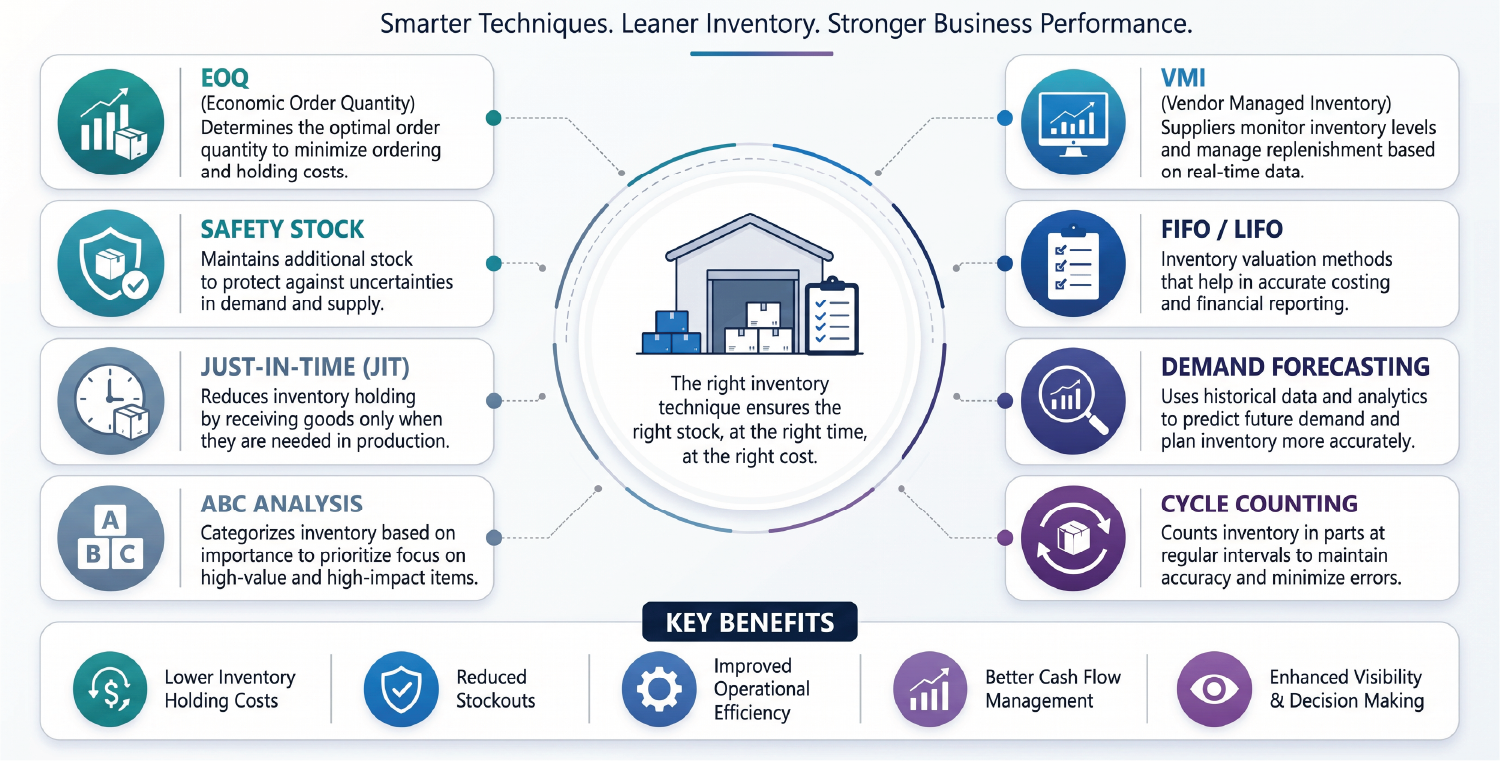
Automates replenishment planning to prevent stock-outs and minimize excess inventory.
Supports accurate financial reporting through valuation methods such as FIFO, moving average, and standard costing.
Strengthens internal controls with transparent inventory records and audit-ready documentation, along with quantity and value.
Aligns stock levels with anticipated demand to improve service levels and reduce carrying costs.
Integrates stage-wise inspection processes to ensure only approved materials enter production or distribution; otherwise, it will go for Non-Conformance (NC) and disposition.
Ensures precise component allocation for production and assembly operations.
Streamlines return processing while maintaining accurate inventory adjustments.
Captures additional costs such as freight, duties, and insurance to determine true inventory value.
It ensures that the right material is available at the right time to meet production and inventory demands. By accurately forecasting supply and demand, organisations can calculate material requirements effectively, thereby avoiding excess stock or shortages. This improves overall operational efficiency and enables smoother supply chain operations.
It is a system-driven process for tracking products in which barcode labels are attached to items stored in the warehouse. These barcodes are scanned during every stock movement, ensuring accurate stock identification and real-time updates within the system.
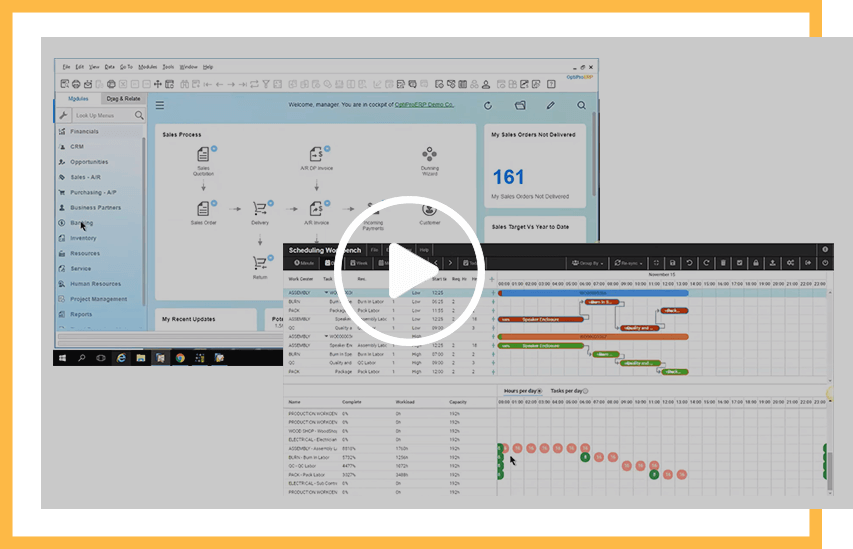
Manufacturing industries often struggle with stock imbalances, which can disrupt production and increase operational costs. Effective inventory management ensures streamlined processes, improved efficiency, and better overall performance. Maintaining optimal stock levels is crucial for achieving high customer satisfaction, minimizing waste, and improving organizational profitability. When inventory management is integrated with the Master Production Schedule (MPS) and the Bill of Materials (BOM), organisations can ensure precise, data-driven material planning. Proper synchronization between MPS, BOM, WMS and real-time inventory data helps businesses avoid:
By leveraging advanced ERP software and intelligent analytics, manufacturers can automate requirement planning and strategically manage excess inventory. Modern ERP systems always optimize stock levels, reduce operational costs, and ensure timely fulfilment of customer demand.
Additionally, advanced stock control methods combined with AI-powered forecasting enhance traceability across the entire supply chain. This enables businesses to make informed decisions, improve supply chain visibility, and achieve long-term operational excellence.
The unpredictable nature of customer demand makes it challenging for manufacturers to maintain optimal inventory levels. Inaccurate demand forecasting often leads to either excess inventory, which increases inventory carrying and storage costs, or stockouts, which can disrupt production schedules, delay customer deliveries, and negatively impact sales performance.
If critical raw material components are out of stock, production lines can come to a complete halt. Even a small missing part can delay the entire production process, disrupt manufacturing schedules, and impact customer delivery commitments. As a result, stockouts can reduce operational efficiency, increase production downtime, and negatively affect overall manufacturing performance.
Many manufacturers struggle with the lack of real-time inventory visibility and continue to rely on outdated inventory records or delayed updates for decision-making. As a result, they may not have an accurate view of available stock across warehouses and production facilities, leading to inventory inaccuracies, poor material planning, production delays, and increased operational costs. Without real-time visibility, maintaining optimal inventory levels and responding quickly to changing production requirements becomes difficult.
External factors such as supplier delays, transportation disruptions, and demand uncertainties can significantly impact material availability across the supply chain. These disruptions make it challenging for manufacturers to maintain consistent production schedules, resulting in material shortages, delayed deliveries, and reduced operational efficiency. As supply chains become increasingly complex and interconnected, manufacturers must proactively manage supply chain risks to minimize disruptions and ensure production continuity.
It is a common challenge in manufacturing because product designs, specifications, and customer requirements frequently change. If demand is overestimated or production is not properly aligned with actual market needs, manufacturers often end up with surplus inventory that moves slowly or does not move at all. Over time, this inventory can become obsolete due to technological advancements, design modifications, or changing customer preferences. Excess inventory also ties up valuable working capital and increases inventory carrying costs such as storage, insurance, handling, and warehouse management expenses. To overcome these challenges, manufacturers leverage real-time demand forecasting, inventory analytics, and ERP systems to identify slow-moving inventory, optimize reorder quantities, improve inventory visibility, and better align production planning with actual customer demand. This helps reduce excess inventory, improve inventory turnover, and enhance overall operational efficiency.
Efficient inventory management is the backbone of any business. Whether you are running a small retail store or a large enterprise, the ability to accurately track and control inventory can significantly impact profitability, operational efficiency, and business growth. Organizations typically rely on one of two approaches: Manual Inventory Management or ERP-Based Inventory Management. While manual methods may be suitable for smaller operations, modern businesses increasingly adopt ERP solutions to gain real-time inventory visibility, improve accuracy, and streamline inventory processes. Let us explore both approaches to understand how they differ and which one is better suited for today’s dynamic business environment.
ERP systems utilize advanced inventory management capabilities that integrate inventory processes with other core business functions such as sales, procurement, production, finance, and warehousing. Unlike manual methods, ERP systems provide real-time inventory tracking, automated updates, and centralized data visibility across the organization. This enables businesses to make faster and more informed decisions based on accurate and up-to-date information. By leveraging data-driven insights, organizations can optimize inventory levels, improve demand planning, reduce stockouts and excess inventory, enhance operational efficiency, and support overall business growth.
| Aspect | Manual Inventory Management | ERP Inventory Management |
|---|---|---|
| Accuracy | Primarily relies on manual methods such as paper records, spreadsheets, or basic software tools, making it more prone to human errors. | Inventory data is automatically maintained and updated within the ERP system, resulting in higher accuracy. |
| Real-Time Updates | Limited or no real-time inventory updates. Information is often updated periodically. | Provides real-time tracking and automated updates of inventory levels across the organization. |
| Efficiency | Time-consuming and heavily dependent on manual labor and data entry. | Streamlines inventory processes through automation, reducing manual effort and improving efficiency. |
| Data Accessibility | Inventory data is often stored locally with limited accessibility and visibility. | Centralized inventory data can be accessed across departments and locations, whether on-premises or in the cloud. |
| Scalability | Suitable for small businesses but becomes difficult to manage as inventory volume and business operations grow. | Easily scales with business growth and can handle increasing inventory complexity and transaction volumes. |
| Cost | Lower initial investment but operational costs increase as the business expands. | Higher initial implementation cost but delivers better long-term ROI through automation and process optimization. |
| Stock Visibility | Limited visibility into inventory levels, movements, and stock availability. | Provides complete visibility into inventory across warehouses, locations, and the entire supply chain. |
| Automation | Minimal or no automation. Most inventory activities are performed manually. | Supports extensive automation, including replenishment planning, reorder alerts, inventory tracking, and reporting. |
| Security | Inventory records can be lost, misplaced, or modified without proper controls. | Offers stronger data security, user access controls, audit trails, and backup mechanisms. |
| Decision-Making | Decisions are often based on assumptions, manual reports, or limited information. | Supports data-driven decision-making through real-time dashboards, analytics, and reporting tools. |
A Tier-2 automotive parts manufacturer experienced significant operational inefficiencies due to fragmented legacy systems that could not support the complexities of high-mix, high-precision manufacturing. Planning, warehouse, and shop floor operations operated in silos, lacking real-time synchronisation and resulting in poor inventory visibility, limited production alignment, and inefficient resource utilisation.
Although the company had adopted Just-In-Time (JIT) and lean manufacturing principles, the absence of integrated planning and real-time inventory validation led to reactive decision-making, frequent production bottlenecks, and ongoing operational challenges. These limitations reduced the organisation’s ability to respond quickly to changing production demands and to maintain optimal inventory levels throughout the manufacturing process.
Recognising the need for a centralised and scalable inventory management solution, the company implemented OptiPro Manufacturing, integrated with SAP Business One, an advanced ERP platform designed specifically for complex manufacturing environments.
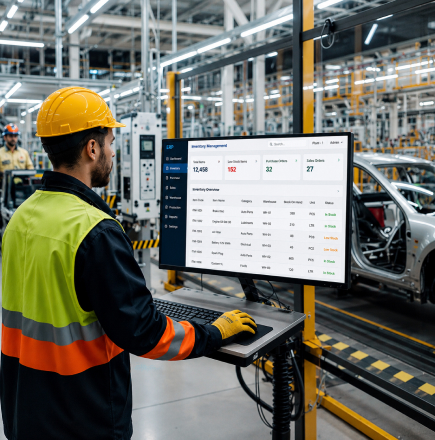
The ERP-based solution streamlined shop floor operations by seamlessly integrating planning, inventory management, and production execution into a unified system. It eliminated reliance on manual data entry and spreadsheets by enabling real-time inventory tracking, automated data synchronisation, and accurate inventory validation. This enabled greater visibility into material availability, production status, and inventory movements across the organization.
As a result, the manufacturer established a connected, data-driven operational framework that improved production efficiency, enhanced inventory accuracy, reduced operational bottlenecks, and strengthened overall control across manufacturing operations.
The transformation initiative focused on synchronizing four critical components of manufacturing operations:
By integrating MPS and BOM directly with live inventory data, the OptiPro Manufacturing system automated previously manual workflows. This eliminated reliance on spreadsheets and reduced human intervention, improving both accuracy and operational speed.
The OptiPro Manufacturing solution introduced powerful automation and intelligent planning features, including:
Through synchronized planning and execution, the company significantly improved its inventory reduction methods without disrupting Just-in-Time (JIT) manufacturing practices. The OptiPro Manufacturing enabled environment provided a clear answer to a common manufacturing challenge: how to reduce inventory without affecting production efficiency. By leveraging data-driven planning, automated replenishment, and accurate material tracking.
The organization was able to:
The implementation of OptiPro Manufacturing, integrated with SAP Business One, transformed fragmented operations into a synchronized, automated, and data-driven manufacturing ecosystem. By integrating critical functions such as Bill of Materials (BOM) management, Warehouse Management System (WMS), Master Production Scheduling (MPS), and inventory management, the manufacturer achieved greater operational visibility and process alignment across the organization. This integrated approach improved production efficiency, optimized inventory utilization, strengthened cost control, and enhanced decision-making capabilities. As a result, the company established a scalable foundation for sustainable operational excellence while remaining competitive in the demanding automotive supply chain.
OptiPro Manufacturing is an integrated inventory control and manufacturing solution designed specifically for discrete manufacturers, providing real-time visibility into raw materials, work-in-progress (WIP), finished goods, and component inventory across the entire production lifecycle. Integrated with SAP Business One, the solution enables manufacturers to seamlessly align inventory management with critical manufacturing functions, including Bill of Materials (BOM), Warehouse Management System (WMS), Master Production Scheduling (MPS), Material Requirements Planning (MRP), routing operations, and production execution.
The platform supports real-time inventory tracking through barcode, batch, serial number, pallet, and bin-level management, ensuring complete inventory accuracy and traceability across warehouses and shop floor operations. Advanced planning capabilities such as forward and backward scheduling, resource allocation, capacity planning, and production order management help manufacturers synchronize material availability with production requirements.
OptiPro Manufacturing also provides inventory visibility through automated stock tracking, monitoring of inventory movement, and real-time synchronisation across warehouse, procurement, and production processes. This enables manufacturers to optimize inventory levels, reduce excess stock, prevent material shortages, and improve production continuity.
By connecting inventory management with production planning, quality control, warehousing, and financial operations, OptiPro Manufacturing helps organizations improve inventory accuracy, increase operational efficiency, strengthen supply chain visibility, reduce inventory carrying costs, and support data-driven decision-making. The result is a connected manufacturing environment that enhances productivity, improves resource utilization, and ensures a smooth and efficient production flow across the enterprise.